Chemical Storage Heaters
Safe and reliable heating for chemical containers
Chemical storage heaters are essential for maintaining the stability and integrity of chemical containers in industrial environments. These heaters provide controlled and consistent heat to prevent freezing, maintain viscosity, or support chemical processes. Sourcing high-quality chemical storage heaters ensures safety, compliance, and operational efficiency. Buyers often look for heaters that are compatible with various container types, offer precise temperature control, and meet international safety standards. Whether for cold climates or process applications, chemical storage heaters play a crucial role in chemical management and transportation.
Main Types & Common Specifications
Electric Drum Heaters
Designed for heating individual chemical drums, these heaters use electric resistance to provide uniform warmth and prevent product solidification.
Steam Jacketed Heaters
Ideal for large-scale operations, these heaters use steam to maintain temperature in chemical storage tanks, offering efficient and scalable heating solutions.
Thermostatic Heaters
Equipped with built-in thermostats, these heaters automatically adjust temperature to ensure optimal performance and energy efficiency.
Insulated Container Heaters
Specifically designed for transport containers, these heaters protect chemicals during transit by maintaining stable internal temperatures.
Infrared Heaters
Offer rapid and targeted heating for chemical storage areas, ideal for spot heating and quick temperature adjustments.
Explosion-Proof Heaters
Built for hazardous environments, these heaters are certified to prevent ignition of flammable vapors, ensuring compliance with safety regulations.
Portable Chemical Heaters
Compact and mobile, these heaters are suitable for temporary heating needs in warehouses, labs, or field operations.
Key Purchasing Considerations
- Compliance with international safety and quality standards
- Compatibility with different chemical container types and sizes
- Energy efficiency and operating costs
- Durability and resistance to chemical corrosion
- Ease of installation and maintenance
- Temperature control accuracy and reliability
Related Products
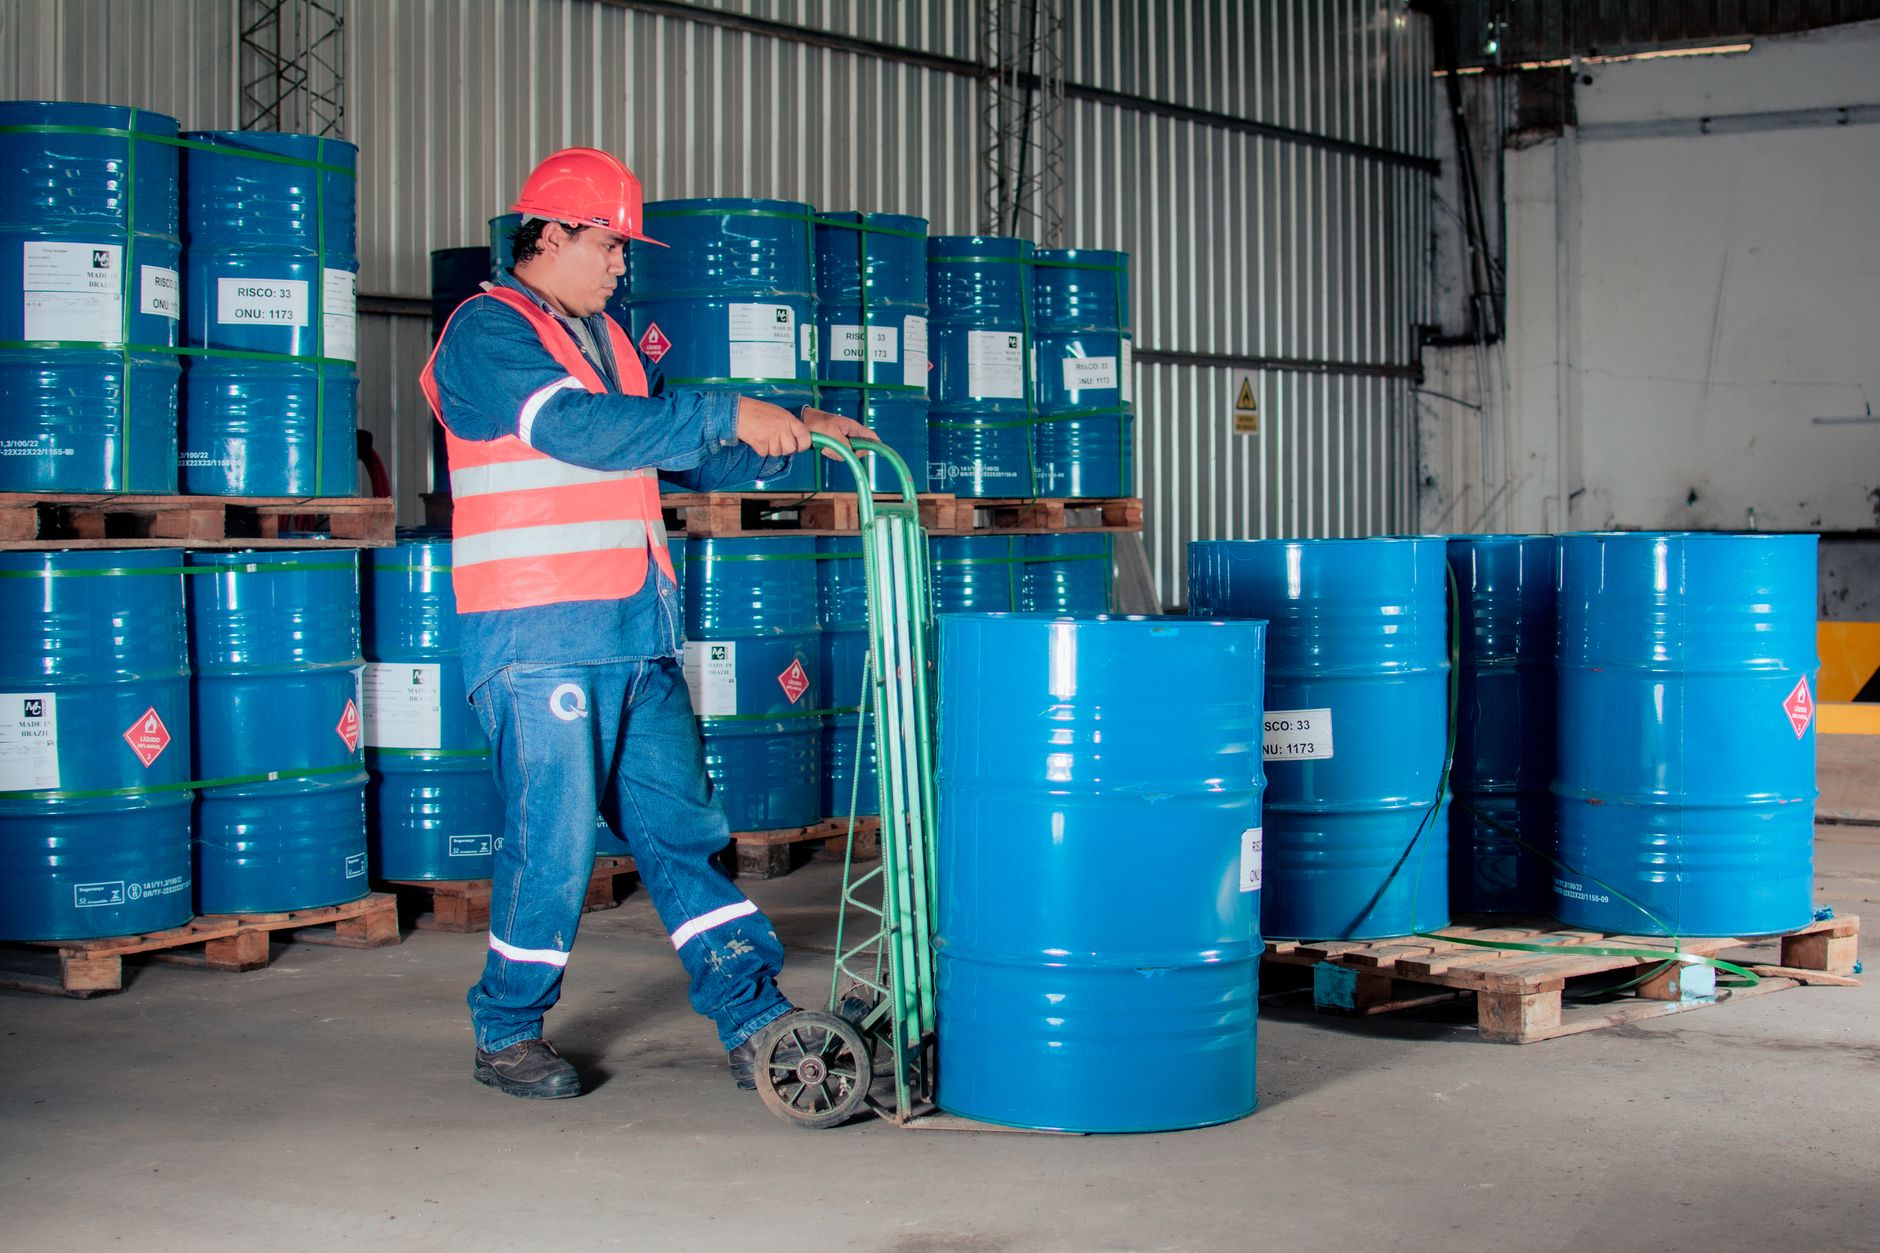
Portable Chemical Storage Heater
Reliable portable chemical storage heater with strict quality control and verified global suppliers for safe, efficient industrial use.
Chemical Storage Heaters
Compact Chemical Heater
Find reliable Compact Chemical Heaters at competitive prices. Learn how to negotiate cost drivers and optimize your sourcing strategy for industrial use.
Chemical Storage Heaters